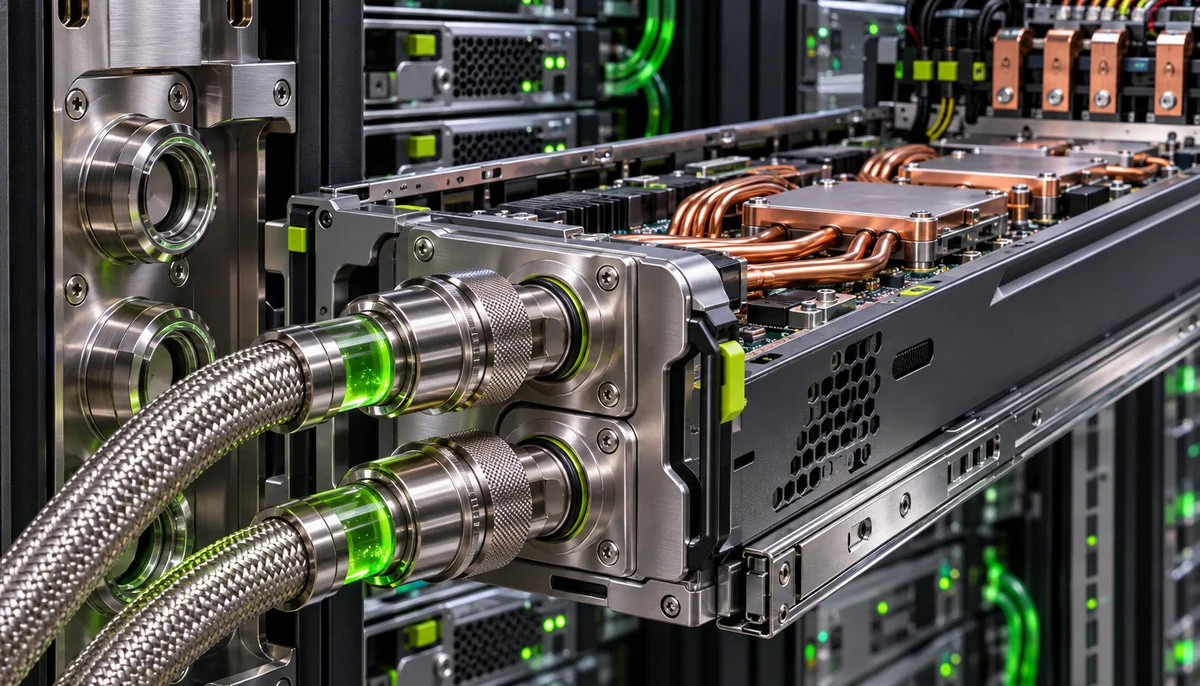
Architectural Shift: Manual Hoses vs. Blind-Mate Rack Manifolds in AI Densities Exceeding 120kW
The thermal dissipation demands of multi-megawatt AI clusters have fundamentally invalidated legacy manual liquid cooling connections. Deployments of NVIDIA NVL72 and high-TDP accelerator architectures concentrate up to 132kW of thermal load within standard EIA-310 and Open Rack v3 (ORV3) footprints, demanding continuous coolant distribution to dozens of independent compute sleds. Manual push-to-connect quick disconnects (QDs) rely on flexible rubber or PTFE braided hoses positioned within high-congestion front or rear service channels. This topology introduces structural operational risk: field technicians frequently induce torsional strain, localized hose kinking, and uneven bend radii during hot-swap operations, leading to premature inner liner fatigue, flow degradation, and particulate release into microchannel cold plates. Furthermore, the manual de-latching of pressurized supply and return loops during unscheduled compute tray servicing enforces a Mean Time to Repair (MTTR) ranging from 45 to 60 minutes per incident.
Blind-mate direct-manifold interfaces transition the hydraulic interconnect entirely to the mechanical chassis backplane, eliminating flexible service loops within the compute envelope. Under the OCP ORV3 liquid cooling specification, male and female hydraulic coupler pairs are rigidly mounted to vertical supply/return fluid distribution headers and compute chassis rear bulkheads, respectively. When a 30kg to 80kg compute tray slides along standardized rolling guide rails, mechanical guide pins achieve kinematic pre-alignment prior to physical hydraulic engagement. This architecture reduces human error vectors during maintenance, ensures invariant insertion vectors, and drops compute tray MTTR to under 5 minutes. The elimination of manual hose routing simultaneously recovers up to 15% of the chassis rear cross-sectional area, directly reducing hydraulic bypass interference and optimizing thermal exhaust pathways for secondary air-cooled voltage regulator modules (VRMs).
Verify compute sled chassis rails provide dual-stage dampening to arrest kinetic shock prior to initial guide pin contact.
Ensure fluid backplane distribution headers maintain rigid structural bracing capable of resisting collective insertion thrust without frame deflection.
Confirm clearance margins within chassis rear envelopes satisfy OCP ORV3 spatial keep-out zones for secondary power busbars.
Validate operational MTTR reduction metrics through instrumented hot-swap service simulations on live production racks.
Mechanical Tolerance Budgets, Kinematic Float, and Insertion Force Dynamics
In a 48U rack housing up to 36 dual-tray server nodes, the structural cumulative tolerance stack-up represents a complex mechanical challenge. Thermal expansion gradients across rack vertical uprights, differential sheet-metal deflection under uneven payload distributions, stamping variations, and seismic transport loads yield cumulative radial misalignments reaching ±2.5mm to ±4.0mm and angular deviations up to ±1.5°. Rigid coupling interfaces subjected to these boundary conditions generate severe mechanical binding, localized galling along the valve sleeve, premature lip-seal deformation, and catastrophic failure of chassis latch mechanisms. To accommodate this dimensional divergence, blind-mate coupling assemblies incorporate multi-axis floating mechanisms, typically implemented on the manifold-side receiver via spring-loaded gimbaled floating plates paired with low-friction fluoropolymer sliding surfaces.
The mechanical alignment sequence operates across three discrete kinematic stages: gross alignment via lead-in chamfers on chassis guide pins, radial self-centering via the floating plate assembly, and final micro-alignment through internal spherical nose-cones on the coupler shell. Mechanically, the total insertion force per compute tray—encompassing both supply and return connectors—must be constrained to $F_{insertion} < 180\text{ N}$ to comply with single-operator ergonomic thresholds and prevent chassis latch buckling. This force profile is governed by the equation: $$F_{insertion} = 2 \times \left( F_{spring} + F_{fluid} + F_{friction} \right)$$, where $F_{spring}$ represents internal poppet return spring compression, $F_{fluid} = P_{supply} \cdot A_{valve}$ is the hydraulic hydrostatic backpressure acting over the effective valve cross-sectional area $A_{valve}$ at nominal system pressure $P_{supply}$ (typically 3.0 to 4.0 bar), and $F_{friction}$ accounts for the dynamic drag of elastomeric radial seals across hard-anodized or passivated mating interfaces.
Measure total multi-axis radial float envelope ensuring a minimum compliance of ±3.5mm along both X and Y axes.
Quantify coupler angular compliance to ensure complete sealing integrity at a sustained misalignment of ±1.2 degrees.
Calibrate tray insertion force using load-cell telemetry to ensure peak thrust remains strictly below 180 N under full hydraulic pressure.
Inspect gimbaled spring return mechanisms to verify zero-backlash return to central resting datum post-extraction.
Hydraulic Performance: Pressure Drop ($ΔP$), Cavitation Prevention, and Flow Balancing
Hyperscale AI deployments require tight volumetric flow rate distributions, typically demanding between 2.0 and 3.5 Liters per Minute (LPM) per compute tray to sustain silicon junction temperatures ($T_j$) below 75°C under continuous 1,000W+ accelerator TDPs. The hydraulic resistance of the blind-mate connector pair constitutes a significant fraction of the total secondary loop head loss. The relationship between flow rate $Q$, flow coefficient $C_v$, and localized pressure drop $\Delta P$ across the mated coupling is expressed by: $$\Delta P = SG \cdot \left( \frac{Q}{C_v} \right)^2$$, where $SG$ is the specific gravity of the coolant (approximately 1.03 for a 25% Propylene Glycol / 75% Deionized Water mixture at 45°C). To prevent excessive pumping power overhead and preserve overall rack Energy Efficiency Ratio (EER), the differential pressure across a mated pair must be maintained at $\Delta P \le 0.18\text{ bar}$ at nominal 3.0 LPM flow, dictating a minimum flow coefficient of $C_v \ge 1.45$.
Streamlining fluid streamlines inside the internal poppet and sleeve geometries is essential to suppress recirculation eddies and localized velocity peaks. Fluid velocities inside the coupler bore exceeding 2.5 m/s generate turbulent boundary layer detachment, inducing localized static pressure drops that can breach the fluid's saturation vapor pressure $P_v$. This condition triggers localized micro-cavitation: $$P_{local} \le P_v(T) \implies \text{Vapor Cavity Inception}$$, leading to implosion-driven acoustic vibration, micro-pitting of metallic structural surfaces, and elastomeric seal erosion. Maintaining the Net Positive Suction Head Margin ($NPSH_{margin} = NPSH_a - NPSH_r > 0.5\text{ bar}$) across the furthest vertical compute tray in a 72-tray manifold requires balancing supply manifold diameters (typically $\ge 1.5$ inches / 38.1mm ID) and optimizing internal valve contours via computational fluid dynamics (CFD) to enforce laminar-like transition profiles through the annulus.
Perform baseline pressure drop testing across mated pairs at 2.0, 3.0, and 4.0 LPM to validate that Delta-P does not exceed 0.20 bar.
Conduct CFD acoustic and velocity gradient analysis to verify internal fluid path velocity remains below 2.2 m/s.
Audit manifold vertical pressure gradients to guarantee uniform fluid distribution within ±5% across all 36 chassis tiers.
Verify Net Positive Suction Head available (NPSHa) exceeds pump vendor requirements by at least 0.5 bar under peak coolant temperatures.
Tribology, Metallurgy, and Elastomeric Seal Degradation Dynamics
The metallurgical and chemical selection for blind-mate quick disconnects is critical to long-term operational reliability over a standard 5-to-7-year server lifespan. AI secondary cooling loops predominantly utilize a 25/75 Propylene Glycol-Deionized Water mix (PG25) enriched with advanced azole-based organic corrosion inhibitors, operating between 15°C and 65°C. The internal wetted metallic components of the coupler must be machined from fully passivated AISI 316L (UNS S31603) austenitic stainless steel or electroless nickel-plated brass (ENP with minimum 25μm thickness and high phosphorus content >10%). 316L is favored due to its resistance to pitting and crevice corrosion, exhibiting a Pitting Resistance Equivalent Number (PREN) $\ge 23$: $$\text{PREN} = \%\text{Cr} + 3.3(\%\text{Mo}) + 16(\%\text{N})$$. Direct contact between dissimilar metals, such as coupling stainless steel and compute tray aluminum structural brackets, must be electrically decoupled via non-conductive dielectric isolation sleeves to keep galvanic potential differences below 150 mV.
Polymeric seal engineering represents the most frequent origin of latent hydraulic failure. Elastomeric O-rings and primary radial wiping seals within the coupler face continuous dynamic shear stresses and chemical attack. Peroxide-cured Ethylene Propylene Diene Monomer (EPDM) is the primary elastomeric compound for PG25 systems, exhibiting low swell (<3%) and high resistance to glycol cross-link cleavage. In contrast, standard bisphenol-cured Fluoroelastomers (FKM) suffer from amine and alkaline corrosion-inhibitor degradation, resulting in progressive embrittlement and micro-cracking. Seal failure modes are governed by compression set and plastic deformation over thermal aging cycles, characterized mathematically by the Maxwell-Wiechert viscoelastic relaxation model: $$\sigma(t) = \epsilon_0 \sum_{i=1}^n E_i e^{-t/\tau_i}$$. If the residual contact pressure of the primary O-ring falls below the operational fluid pressure ($P_{contact} < P_{coolant}$), seal bypass leakage occurs. Furthermore, dynamic pressure pulsations generated by pump rotation must not induce O-ring extrusion into the clearance gap, demanding seal hardness ratings of 75 to 85 Shore A combined with PTFE anti-extrusion backup rings.
Specify passivated AISI 316L stainless steel for all wetted internal metallic components, verifying ASTM A967 chemical passivation compliance.
Mandate peroxide-cured EPDM compounds certified for continuous operation up to 105°C with less than 15% compression set after 1,000 hours.
Inspect coupling mechanical interfaces to ensure anti-extrusion PTFE back-up rings are positioned on the downstream pressure side of all elastomeric seals.
Validate fluid-material compatibility matrix to eliminate copper-alloy catalytic oxidation in the presence of deionized water matrices.
Spill-Free Dry-Break Architectures and Active Leak Detection Protocols
To protect high-voltage power distribution networks (e.g., ORV3 48V/400V busbars) located directly adjacent to hydraulic headers, blind-mate couplers must utilize true flush-face dry-break poppet designs. During the uncoupling sequence, the internal fluid passages within both the male probe and female socket must close fully before the primary dynamic seals unseat from their corresponding interfaces. This sequencing restricts air inclusion into the operational cooling loop to $V_{air} < 0.10\text{ ml}$ per disconnect event and limits liquid spillage to $V_{fluid} < 0.05\text{ ml}$ (a microscopic fraction of a droplet). The flush-face geometry presents a flat, easily cleanable external interface that minimizes particulate accumulation when a compute tray is removed for maintenance, preventing debris ingress into the manifold during subsequent re-insertion.
Even with ultra-low-spill mechanical couplers, hyperscaler risk frameworks require active, autonomous containment protocols integrated into the rack architecture. Localized drip trays positioned immediately below the vertical manifold coupling junctions channel any micro-leakage toward dedicated diagnostic reservoirs. These catch basins integrate dual-technology leak detection: high-sensitivity conductive polymer sensor ropes cross-referenced with optical refractive liquid level sensors. Upon liquid detection, the rack's localized micro-controller triggers an emergency fault interrupt across the Centralized Coolant Distribution Unit (CDU), commanding the closure of fast-acting rack-level isolation solenoid valves in $t < 50\text{ ms}$. This sub-second isolation halts primary pumping loops, depressurizes the supply manifold via secondary bypass return channels, and isolates electrical power domains to prevent catastrophic flashover across adjacent high-current power interconnects.
Verify disconnect fluid spillage remains strictly below 0.05 ml across 50 consecutive disengagements under 3.5 bar fluid pressure.
Inspect flush-face sealing surfaces to ensure zero exposed cavity gaps capable of harboring atmospheric particulate accumulation.
Calibrate dual-technology leak detection circuits, verifying sensor trip-to-solenoid actuation latency occurs in under 50 milliseconds.
Conduct simulated droplet containment tests to confirm drip tray geometries direct fluid away from busbar infrastructure under maximum airflow draft.
Commissioning Verification, Automated In-Line QC, and Cleanliness Standards
Field commissioning and factory quality control of liquid-cooled hyperscale racks require multi-stage non-destructive testing protocols prior to shipping and energization. Every assembled manifold and blind-mate coupling sub-assembly must undergo Helium Mass Spectrometer Leak Detection in accordance with ASTM E499 methodology. The component is evacuated to an absolute vacuum level of $P_{abs} < 1\text{ mbar}$, backfilled with a 10% Helium / 90% Dry Nitrogen tracer gas to 1.5 times the Maximum Allowable Working Pressure ($1.5 \times \text{MAWP} = 6.0\text{ bar}$), and tested inside a vacuum chamber. The maximum permissible helium leak rate is strictly defined as $Q_{He} \le 1.0 \times 10^{-6}\text{ mbar}\cdot\text{L/s}$. Accelerated life cycle stress testing protocols dictate that couplers must sustain a minimum of 500 complete mechanical mate/demate cycles under continuous working pressure and maximum specified angular misalignment without exceeding base leakage thresholds.
Particulate contamination within the hydraulic loop represents a primary failure mode for both cold plates and blind-mate couplings, as particulates trapped on valve sealing seats breach seal integrity. Production cooling loops must comply with rigorous cleanliness metrics governed by ISO 4406 and NAS 1638 standards. Prior to deployment, fluid distribution manifolds must undergo turbulent flushing regimes achieving a Reynolds number $Re \ge 4000$ through a 5-micron absolute filter until the particulate concentration meets or exceeds ISO 4406 Class 16/14/11 (NAS Class 5 equivalent). The presence of metallic burrs, swarf, or elastomeric shedding larger than $25\mu m$ is categorized as a critical defect capable of wedging internal sliding sleeves, invalidating dry-break poppet return strokes, and triggering catastrophic post-commissioning coolant release.
Execute helium mass spectrometry testing on all coupling assemblies, certifying leakage remains under 1.0 x 10^-6 mbar*L/s at 6.0 bar proof pressure.
Subject pilot production samples to 500 mechanical endurance cycles under full working pressure to verify seal lip integrity.
Verify flushed manifold loop fluid cleanliness adheres strictly to ISO 4406 class 16/14/11 limits via in-line laser particle counters.
Implement factory end-of-line optical inspection to verify internal sliding sleeves and valve seats are free of foreign particulate debris larger than 10 microns.
Engineering Procurement & Technical Desk
For technical datasheets, custom power topology design, or volume export quotations, reach out to HEFENGQI engineers.